Premium shelf-stable food products engineered for foodservice, supermarket retail, and wholesale distribution in Melbourne.
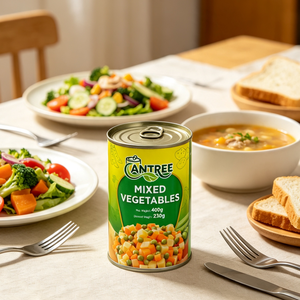
Melbourne stands as Australia's undisputed culinary capital and a critical logistics nexus for Victoria’s regional food networks. Managing the supply chain for high-volume commercial kitchens in Southbank, bustling pizzerias in Carlton, institution-level caterers across Greater Melbourne, and national supermarket distribution centers along the M1/M80 corridors demands absolute reliability, regulatory conformity, and uncompromised food safety. As leading canned food manufacturers and suppliers serving Melbourne, we provide an institutional-grade manufacturing foundation tailored to the strict procurement protocols of Australian buyers.
Navigating modern procurement requires balancing raw ingredient provenance, thermal sterilization efficiency, freight optimization via the Port of Melbourne (Swanson and Victoria Docks), and compliance with the Australia New Zealand Food Standards Code (FSANZ). Our manufacturing infrastructure delivers custom private label (OEM/ODM) formulation and direct contract packing services engineered to insulate commercial partners against market volatility, energy cost inflation, and seasonal supply disruptions.
Full alignment with Standard 1.2.1 to 1.2.10 for food labeling, mandatory allergen declarations, and Country of Origin Labelling (CoOL) frameworks required by Australian Consumer Law.
Optimized 20ft and 40ft High Cube container load factor design, enabling maximum pallet density, zero-breakage transit, and expedited customs clearance via Melbourne intermodal hubs.
Overpressure retort cooking executing precise thermal lethality curves ($F_0 \ge 3.0$), guaranteeing commercial sterility without relying on artificial chemical preservatives or additives.
Canned commodities are no longer categorized merely as emergency pantry reserves; they serve as fundamental baseline components for high-efficiency commercial food prep, retail shelf innovation, and institutional catering operations. Our product portfolio is structured to solve operational challenges unique to Melbourne’s commercial sectors:
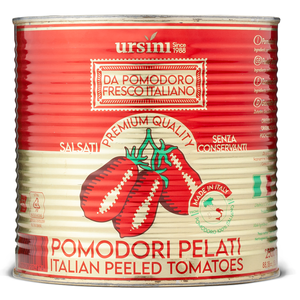
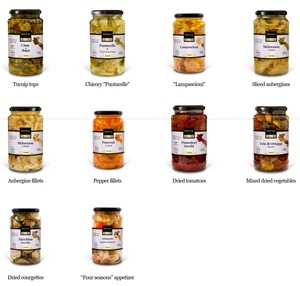
Featured Solution: High Quality Italian Peeled Tomatoes 2.5kg (A10 Can) & Gourmet Antipasto Vegetables.
Melbourne’s famous dining precincts—from Lygon Street in Carlton to Docklands—demand high-viscosity tomato pulp with consistent Brix levels (5.5° to 7.0°) for pizza bases and slow-simmered sauces. Bulk 2.5kg food cans eliminate prep labor while delivering authentic Mediterranean sensory profiles.
Featured Solution: Canned Sweet Corn Kernels 400g & 4-Way Mixed Vegetables (Peas, Carrots, Corn, Beans).
Retail chains across Victoria require high-speed private label turnarounds. Packaged in EOE (Easy-Open End) tinplate cans with customized outer shrink-wrap or shelf-ready packaging (SRP), our lines comply fully with barcode verification and Australian retail packaging standards.
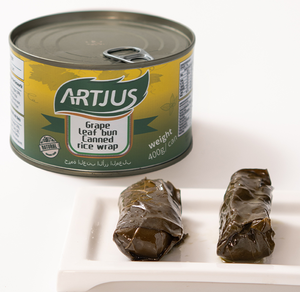
Featured Solution: Canned Brine Stuffed Grape Leaves Rice (Dolmades) 400g & Spina Gourmet Olives.
Servicing vibrant multicultural hubs like Oakleigh, Brunswick, and Coburg. Our authentic grape leaf wrapping, balance of extra virgin olive oil brine, and airtight glass or tin sealing preserve traditional texture without tearing, providing premium shelf appeal for independent delicatessens.
The Victorian food sector is undergoing a structural shift driven by climate variability, fluctuating cold-chain transport costs, and evolving consumer dietary expectations. Procurement teams in Melbourne are increasingly migrating from chilled/frozen formats toward high-grade, shelf-stable thermal processing due to four key industry trends:
Refrigerated freight requires continuous diesel generator usage and energy-intensive warehousing. Hermetically sealed canned foods eliminate zero-point storage power consumption, allowing distributors in Truganina and Altona to reduce logistical carbon footprints by up to 38% per ton shipped.
Victorian health-conscious consumers demand complete transparency regarding packaging materials. Our manufacturing facilities utilize state-of-the-art BPA-NI (Bisphenol A Non-Intent) internal organosol and acrylic coatings, ensuring no chemical migration occurs even with acidic foods like peeled tomatoes or pineapple chunks.
Modern Australian food guide recommendations require lower ambient salt levels. We utilize vacuum-assisted brine injection that achieves commercial preservation while maintaining low sodium profiles (<120mg per 100g), catering to health-focused institutional health care and school catering channels.
Technical benchmarks for commercial purchasing agents, QA managers, and supply chain coordinators evaluating container specs and processing tolerances:
| Product Category | Standard Pack Sizes | Inner Lining Specs | Sterilization Parameters | Shelf Life | Primary Certification |
|---|---|---|---|---|---|
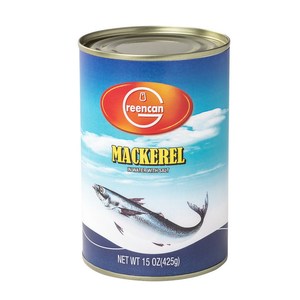
| Canned Seafood (Sardines, Mackerel) | 125g Club, 425g Oval / Tall | Aluminum-Paste Organosol (BPA-NI) | Retort $F_0 \ge 10.0$ min, 121.1°C | 36 Months | HACCP, BRCGS Grade A, Halal |
| Peeled Tomatoes & Sauces | 400g Retail, 2.5kg A10 Industrial | High-Acid Gold Vinyl / Acrylic | Hot Fill + Retort $F_0 \ge 5.0$ min | 24-36 Months | ISO 22000, FSANZ Compliant |
| Fruit in Syrup (Pineapple) | 567g, 850g, 3.0kg Foodservice | White Enamel / Acid Resistant | Atmospheric / Pressure Cooking | 24 Months | BRCGS, Halal, Kosher |
| Vegetable & Legume Mixes | 400g EOE, 2.8kg Catering Can | Modified Epoxy / Polypropylene | Overpressure Retort $F_0 \ge 6.0$ min | 36 Months | Non-GMO, HACCP, BRCGS |
| Gourmet Antipasto (Grape Leaves) | 400g Ring-Pull, Glass Mason Jar | BPA-Free Lacquer / Glass Hermetic | Controlled Thermal Acid Pasteurization | 24 Months | International Standard Food Safety |
As an established global supplier offering integrated OEM, ODM, and private label services, our operation bridges the gap between high-volume overseas production efficiency and local Australian compliance strictness. We take full responsibility for the entire manufacturing pipeline:
Our in-house food technologists work directly with brand owners to engineer exact flavor profiles, Brix levels, drain weights, and viscosity metrics to match proprietary product briefs.
Every single production batch undergoes 14-day incubation testing, double-seam dimensional analysis, micro-biological screening, and physical vacuum checking before COA release.
We supply complete documentation packages—including Certificates of Free Sale, Phytosanitary Certificates, Health Certificates, and Packing Declarations—ensuring zero delays at Australian border controls.
Direct technical answers addressing common questions from purchasing agents, freight forwarders, and brand managers in Victoria:
Whether you are expanding a retail private label brand, sourcing bulk foodservice ingredients for Victoria caterers, or seeking reliable OEM contract manufacturing, our team delivers uncompromised quality and reliable supply chains.
Contact Us