High-protein kibbles, functional treats, freeze-dried micronutrient matrices, and veterinary-grade supplements produced under strict ISO/GMP quality protocols.
The global market for pet nutraceuticals and fortified foods has shifted from simple dietary supplementation to highly complex, clinical-grade nutritional intervention. Modern pet owners actively demand targeted functional health outcomes—ranging from joint mobility and gastrointestinal microbiome regulation to cognitive decline prevention and dermatological management. Consequently, procurement officers, brand owners, and veterinary distributors must scrutinize manufacturing partners through a multi-dimensional framework of technical competence, nutrient stability preservation, and stringent regulatory compliance.
When contracting a manufacturer for pet vitamins, soft chews, premixes, or fortified kibble, evaluating pure unit price without assessing batch integrity and thermal degradation protection represents a significant risk. The technical integrity of a pet supplement relies heavily on how vitamins (such as A, D3, E, B-complex, and C) and chelated minerals survive thermal extrusion, retort sterilization, or freeze-drying. Top-tier production facilities employ sophisticated microencapsulation techniques, cold-extrusion technologies, and validated post-extrusion liquid application systems to ensure finished products retain guaranteed analytical constituent potency throughout their entire shelf life.
Heat, moisture, and shear forces during extrusion can destroy up to 60% of unfortified B-vitamins and Vitamin C. Leading factories utilize fat-coated microencapsulated vitamins that remain inert until acted upon by enzymatic breakdown in the small intestine.
High-performance HPLC (High-Performance Liquid Chromatography) testing must be performed on both raw premixes and finished goods to guarantee that statutory label guarantees match physical reality across every commercial batch.
Pet vitamin and soft chew manufacturing lines require environmental controls similar to human pharmaceuticals to prevent microbial contamination, moisture buildup, and premature oxidation of essential fatty acids.
Bridging British nutritional formulation precision with high-capacity global manufacturing to deliver private label solutions without operational friction.
We do not operate merely as an anonymous contract packer. As the team behind acclaimed brands such as Griffiths’ Dog Food®, Clydach Farm®, and Clinigol® Veterinary Science, we test and perfect every manufacturing pipeline on our own commercial labels before offering it to global partners.
Most pet nutrition projects suffer delays due to fragmented suppliers—nutritionists, raw material brokers, extrusion plants, and export clearance agents. We eliminate handoffs by consolidating recipe modeling, pilot trials, packaging compliance, and export health certificates under one roof.
Our standardized development pathway transitions brand briefs into commercial retail-ready pallets in 8 to 16 weeks. This includes FEDIAF/AAFCO nutrient validation, raw material sourcing, trial extrusion runs, palatability testing, and legal packaging artwork sign-off.
| Product Category | Formulation Options | Dosing Format | Compliance & Quality Audit |
|---|---|---|---|
| Functional Soft Chews | Joint (Glucosamine/Chondroitin), Calming, Skin & Coat | Cold-Pressed Soft Chew (2g - 5g) | GMP+, ISO 22000, Micro-Screened Batch Retains |
| Multivitamin Kibble Fortification | Life-stage (Puppy, Adult, Senior), Breed-specific | Extruded Kibble + Vacuum Liquid Coating | FEDIAF Aligned, Post-Extrusion Active Testing |
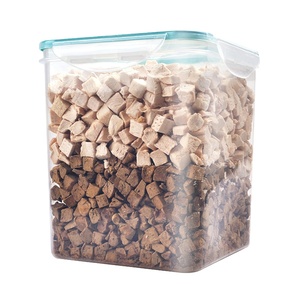
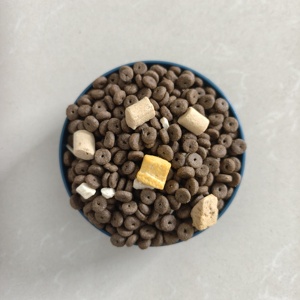
| Freeze-Dried Vitamin Matrices | Single/Multi Protein + Raw Botanical Premixes | Lyophilized Cubes, Treats, or Meal Mixers | Pathogen Free (Zero Salmonella/Listeria), USDA/FDA |
| Clinical & Veterinary Diets | Renal Support, Gastrointestinal Care, Dermatological | Dry Kibble, Wet Pouches, Canned Liquids | Clinigol® Protocol, Full Traceability Certificates |
How technological breakthroughs and changing consumer values are redesigning the landscape of pet dietary supplements and functional foods.
Traditional synthetic vitamin salts suffer from poor absorption and rapid urinary excretion. Advanced factories are integrating liposomal encapsulation, which wraps active vitamins inside phospholipid bilayers. This protects the nutrients from harsh stomach acids, yielding up to 400% higher cellular uptake in canine and feline digestive systems.
The pet wellness market is moving beyond basic live probiotics toward heat-stable postbiotics (inactivated microbial cell mass containing functional metabolites). Combining postbiotics with B-vitamins and soluble dietary fibers creates a synergistic gut-brain-axis supplement that survives shelf-life without refrigeration.
Thermal processing remains the single largest enemy of functional vitamins. The future of kibble production relies on post-extrusion cold-vacuum coating. High-value vitamins, enzymes, and probiotics are infused into the kibble core under negative atmospheric pressure after thermal drying, preventing thermal degradation.
As regulatory scrutiny increases across international jurisdictions (including European Union regulation EC 767/2009, US FDA FSMA guidelines, and Asian importation protocols), procurement directors must adapt their purchasing strategies to guarantee supply continuity and brand protection.
Single-source dependency on active pharmaceutical ingredients (APIs) and vitamin premixes leaves brands vulnerable to geopolitical and shipping shocks. Leading suppliers maintain audited back-up suppliers across Europe, the UK, and North America, ensuring every single vitamin premix element has fully documented origin certificates.
Legacy manufacturing models requiring 20-ton minimum order quantities for custom formulated treats or vitamins are being replaced by modular, flexible production runs. Brand owners now test functional recipes in trial volumes (1 to 3 tons) to validate real consumer demand before committing to full-scale commercial production.
Vitamin supplements are vulnerable to light and oxygen degradation. Modern procurement prioritizes fully recyclable, high-barrier mono-material pouches (PE/PE or PP/PP) with specialized oxygen-scavenging inner layers. This eliminates non-recyclable foil laminates without compromising functional shelf stability.
Clear, definitive answers to operational queries commonly raised by enterprise buyers, brand managers, and import specialists.
MOQs are optimized according to product format. For dry extruded functional kibbles, production is typically scheduled in batch increments of 3 to 5 metric tons to ensure nutrient blending precision. For soft chews, liquid toppers, or packaged vitamin treats, smaller trial runs (starting from 1,000 to 3,000 units) can be accommodated for market testing.
We utilize a two-pronged engineering strategy. First, heat-susceptible micronutrients are introduced via fat-coated microencapsulated premixes that withstand thermal processing. Second, heat-vulnerable bio-actives (such as probiotics, enzymes, and natural Vitamin C) are added post-extrusion using precision cold-vacuum coating equipment.
A complete new product development pipeline takes between 8 to 16 weeks. This includes nutritional modeling, raw material assay validation, pilot trial batches, analytical Constituent testing, statutory artwork compliance checks, and initial commercial production sign-off.
Yes. We regularly export to over 20 global markets across North America, Europe, the Middle East, and Asia-Pacific. Our regulatory team handles export health certificates, sanitary declarations, multi-lingual ingredient panel translations, and container loading optimizations.
Yes. Under our Clinigol® Veterinary Science framework, we formulate and manufacture clinical-grade diets targeting renal care, gastrointestinal sensitivity, dermatological recovery, and weight management with restricted ingredient panels and tight analytical tolerances.
Every raw material ingredient undergoes strict intake verification, including heavy metal, mycotoxin, and microbial screening. Samples from every commercial production run are retained for the duration of the product's shelf-life, providing complete backward traceability from customer retail shelves back to raw material batch codes within hours.
Consult directly with our technical formulation team to discuss custom recipes, pilot trial runs, or scale up your existing private label product portfolio.