Engineered to cGMP, ISO 22000, and FDA specifications with batch-level analytical transparency and global shelf-life stability.
Analyzing global market dynamics, regulatory convergence, and supply chain re-engineering across China’s advanced nutriceutical manufacturing ecosystem.
In the contemporary global dietary supplement and functional food matrix, brand equity is no longer dictated solely by brand marketing; it hinges on pharmaceutical-grade delivery precision, rapid bio-efficacy, clean-label transparency, and total supply chain traceability. Global brand owners, pharmaceutical spin-offs, and clinical nutrition providers are increasingly shifting from simple "white-label catalog off-the-shelf" sourcing toward highly specialized, custom formulation contract manufacturing.
As a leading China Wholesale Custom Formulation Manufacturer & Factory, our industrial infrastructure operates at the intersection of biochemical research, advanced galenic formulation development, and massive scale cost-efficiency. By integrating standardized botanical extraction, synthetic bio-ingredient synthesis, dynamic particle engineering, and novel oral delivery formats under cGMP (Current Good Manufacturing Practice) conditions, we solve the most complex formulation bottlenecks facing modern brand owners.
Overcoming bio-accessibility limits through targeted microencapsulation, liposomal emulsification, and multi-phasic release systems. We turn unstable active pharmaceutical and nutriceutical ingredients into shelf-stable, highly active finished formats.
Every commercial batch produced within our China facilities is accompanied by complete analytical validation datasets, conforming to US FDA 21 CFR Part 111, European Food Safety Authority (EFSA), and international pharmacopeial standards.
By leveraging localized vertical integration—from direct botanical cultivation and extraction to high-speed automated capsule and pouch filling—we minimize unit manufacturing costs without sacrificing chemical integrity.
How cutting-edge oral solid dosage and alternative delivery formats are redefining consumer compliance and therapeutic potency.
Traditional hard tablets and softgels are experiencing market saturation. The modern global consumer demands sublingual absorption, sustained multi-stage release profiles, and instant onset active ingredients. Our plant-level engineering focuses heavily on solvent-free oral pouches and multiphasic capsule-in-capsule technology.
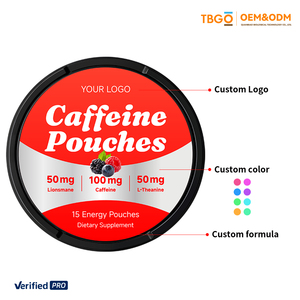
First popularized in energy and nicotine delivery, buccal pouch technology represents a major frontier for nutriceuticals. By eliminating gastrointestinal degradation and hepatic first-pass metabolism, actives such as anhydrous caffeine, NMN, and L-theanine deliver immediate physiological action.
Manufacturing Benchmark: Micro-perforated non-woven food-grade fabric with precise moisture-bound microencapsulated actives, guaranteeing zero powder leakage and uniform dissolution profiles.
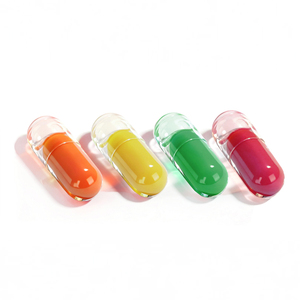
Capsule-in-capsule technology resolves complex ingredient incompatibility issues. An inner solid capsule containing sensitive probiotics or botanicals is suspended inside an outer liquid hard shell packed with lipophilic lipid carriers (e.g., Omega-3, Vitamin D3, or MCT Oil).
Manufacturing Benchmark: Nitrogen-purged hermetic sealing prevents oxidation, enabling 24-month room temperature potency survival for dual hydrophilic and lipophilic actives.
Modern sports and clinical hydration powders demand exact osmolality balance. Custom formulations require granular micronization to achieve instant cold-water solubility without clump formation, utilizing low-glycemic, keto-compatible carrier systems like polydextrose and erythritol.
Manufacturing Benchmark: Agglomeration and instantization technologies that optimize bulk density and flowability for high-speed automated stick-pack lines.
Best practices for brand owners navigating contract manufacturing sourcing from China to ensure quality, IP security, and uninterrupted delivery timelines.
Robust supply chains require multi-vendor qualification. As a strategic OEM/ODM factory, we utilize a dual-sourcing model for core active raw materials (such as Creatine Monohydrate, Botanical Extracts, and Amino Acids), ensuring supply resilience against regional climate impacts or supply shortages.
Confidentiality is paramount when outsourcing proprietary formulation recipes. We implement strict IP protection protocols, including compartmentalized master batch production records (MBRs) where sensitive active proportions remain sealed within isolated cleanroom zones.
Global buyers are systematically rejecting synthetic lubricants like magnesium stearate and titanium dioxide. Our R&D formulation laboratory specializes in replacing traditional excipients with natural rice hull extracts, organic tapioca maltodextrin, and natural fruit concentrates.
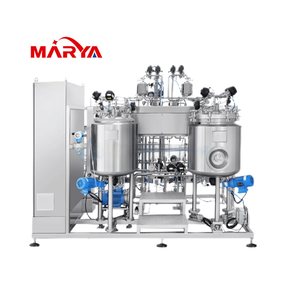
Inside our Marya Professional Formulation Systems: Complete oversight from raw material intake to sealed export pallets.
We run dedicated 5kg to 50kg pilot lines for R&D testing before scaling to full 2,000kg commercial production batches. This guarantees kibble, capsule, or pouch integrity, flavor profile acceptance, and analytical constituent verification.
Our in-house analytical testing suites are equipped with High-Performance Liquid Chromatography (HPLC), Gas Chromatography-Mass Spectrometry (GC-MS), Atomic Absorption Spectroscopy (AAS), and rapid FT-NIR raw material identification units.
Exporting dietary supplements and functional formulations requires specialized documentation. We manage health certificates, Certificate of Free Sale (CFS), allergen statements, customized multilingual labeling, and container temperature monitoring.
Addressing technical, operational, and commercial questions commonly raised by brand procurement teams and technical directors.
MOQs depend directly on the delivery format and packaging configuration. For standard powder formulations (such as Creatine, Protein, or Electrolyte powders), MOQs typically start at 500 kg to 1,000 kg per flavor variant. Specialized oral energy pouches and liquid-filled dual capsules start at 100,000 pouches or capsules per production run. Small-scale pilot batches can be arranged during the R&D stage for market validation.
We provide two procurement models: 1) Full turnkey sourcing through our qualified tier-1 supply network, or 2) Client-supplied active ingredients. Every raw material entering our warehouse undergoes Fourier-Transform Near-Infrared (FT-NIR) spectroscopy identification, microbiological analysis, heavy metal screening (ICP-MS), and HPLC active constituent assay testing prior to cleanroom release.
A typical end-to-end development cycle takes between 8 and 14 weeks. This includes: 2 weeks for bench formulation modeling and sample sign-off; 3–4 weeks for raw material procurement and analytical lab validation; 2 weeks for cleanroom batch production and primary/secondary packaging; and 1–2 weeks for final QC release testing, certificate generation, and container staging.
Yes. Our infrastructure includes isolated production lines capable of manufacturing veterinary-led nutritional supplements, clinical care powders, and specialized botanical extracts. We adhere strictly to cross-contamination prevention guidelines, utilizing validated CIP (Clean-in-Place) systems between distinct batch runs.
We conduct both accelerated stability testing (40°C ± 2°C / 75% RH ± 5% RH for 6 months) and real-time long-term stability testing (25°C ± 2°C / 60% RH ± 5% RH) following ICH guidelines. Complete stability analytical reports are provided to support regulatory registration with global authorities such as the US FDA, European EFSA, and GCC authorities.
Botanical natural variability is controlled through standardized TLC fingerprinting and HPLC quantification of marker compounds. We adjust extraction parameters (temperature, pressure, solvent ratio) to normalize active phytocompound concentration across varying crop harvests, guaranteeing consistent potency on every finished product label.
Partner with China's premier wholesale custom formulation manufacturer. Connect directly with our formulation scientists and B2B contract production directors today.