Engineered for maximum bio-solubility, precise amino acid profiling, and stringent compliance with EU Regulation, FDA standards, and global quality benchmarks.
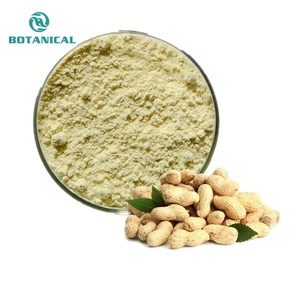
Cold-pressed plant extraction featuring >85% protein concentration, superior dispersibility, and zero chemical residues. Ideal for clean-label beverage and food processing.
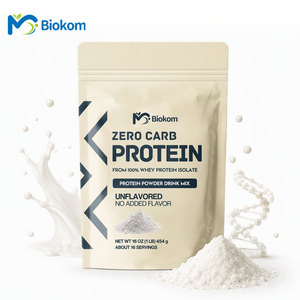
Ultra-filtered WPI 90+ featuring zero lipid retention, enriched electrolyte profiles, and rapid cellular absorption designed for clinical and sports nutrition recovery systems.
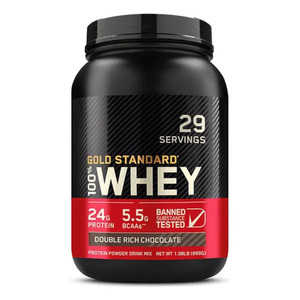
Tailor-made athletic nutrition matrices combining whey concentrate, branched-chain amino acids (BCAA), and digestive enzyme complexes for maximum muscle protein synthesis.
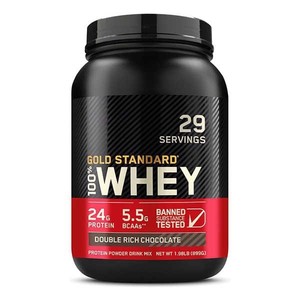
Commercial retail-ready formulation in 1.98LB (899g) packaging. Exceptional palatability, instantized mixability, and rigorously verified analytical purity.
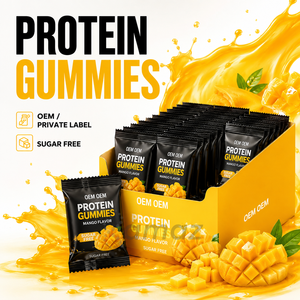
Breakthrough confectionery matrix delivering micro-encapsulated protein per gummy bear without thermal degradation. Zero added sugar with natural fruit flavoring.
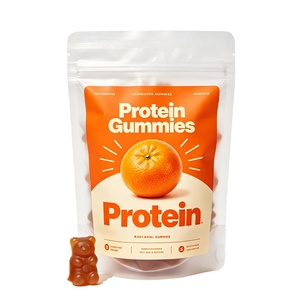
Pre-workout active delivery system combining hydrolysed whey isolate, bio-available creatine monohydrate, essential electrolytes, and natural caffeine for targeted energy boosts.
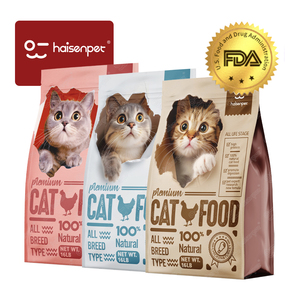
High-meat kibble engineered via low-temperature thermal extrusion. Tailored nutrient density, single-protein transparency, and optimized physical kibble geometry.
Sublimation freeze-dried raw protein matrix designed for sensitive stomachs, gut microbiome support, and dermal health across all life stages.
Operating state-of-the-art facilities equipped for high-protein extraction, micro-encapsulation, freeze-drying, and precision extrusion under strict quality frameworks.
Every single batch produced across our facility undergoes rigorous intake verification, NIR spectroscopy monitoring, and end-to-end analytical testing. Raw materials are audited back to primary sources, ensuring total elimination of heavy metals, micro-contaminants, or unverified adulterants.
Our proprietary manufacturing system records thermal curves, moisture migration parameters, and particle size distribution in real time, granting institutional clients unprecedented quality audit confidence.
As the primary manufacturing force behind recognized high-spec lines such as Griffiths’ Dog Food®, Clydach Farm®, and Clinigol® Veterinary Science, our white-label solutions aren't theoretical—they are battle-tested in demanding international consumer and clinical channels.
We apply identical quality assurance standards, batch tolerances, and regulatory documentation checks to client private-label products as we do to our own award-winning portfolio.
Navigating global compliance requires precise technical mastery. Our facility is fully certified under European Conformity (CE) parameters, aligning with FEDIAF, EFSA, ISO 22000, and FDA standards.
We provide comprehensive export documentation, health certification, veterinary health passports, and legal artwork verification for seamless cross-border logistics across Europe, North America, the Middle East, and Asia.
| Processing Vector | Technical Capability Range | Quality Benchmark Standard | Primary Industrial Application |
|---|---|---|---|
| Spray Drying & Micro-Encapsulation | Particle sizes: 80 - 250 mesh; Temp control < 45°C active core | Zero protein denaturing; Retention of functional bioactive peptides | Instantized Whey Isolates, Functional Gummies, Plant Extracts |
| Low-Temperature Extrusion | Moisture adjustment: 8% - 12%; Pressure control 15-35 Bar | Maillard reaction minimization; Max retention of thermolabile vitamins | High-Meat Pet Foods, Veterinary Diets, Specialized Kibbles |
| Sublimation Freeze-Drying | Vacuum pressure < 0.1 mbar; Ice sublimation >99.2% moisture removal | Cellular structural preservation; Complete raw pathogen reduction | Raw Freeze-Dried Cat & Dog Treats, Biological Extracts |
| Enzymatic Hydrolysis | Degree of Hydrolysis (DH): 5% - 25%; Molecular weight < 3000 Da | Hypoallergenic profile; Rapid intestinal mucosa absorption | Clinical Veterinary Diets, Post-Workout Recovery Supplements |
Market intelligence for B2B procurement managers, brand directors, and distribution networks preparing for the next decade of protein consumption dynamics.
Procurement demands have migrated away from crude protein content percentages toward bio-availability and digestibility metrics (PDCAAS and DIAAS scores). Buyers now prioritize enzymatic hydrolysis, which breaks dense protein chains into short-chain di- and tri-peptides.
This shift dramatically enhances mucosal absorption rates, reduces gut hypersensitivity, and allows brands to claim clinical-grade efficacy in both human functional sports supplements and veterinary diet solutions.
Traditional capsules and heavy powders are experiencing market saturation. The fastest-growing category in sports and lifestyle nutrition is high-protein functional gummies.
Overcoming historical thermal degradation challenges, advanced factories utilize cold-set pectin and starch-molding technologies. This enables the inclusion of 20-30% active whey isolate or creatine monohydrate per gummy without compromise to texture or shelf stability.
As consumer sensitivity to multi-ingredient allergen profiles increases, demand for single-source plant extractions—such as cold-extracted, water-soluble peanut protein and yellow pea isolate—is surging.
Procurement teams are prioritizing suppliers who can guarantee non-GMO origin, chemical-solvent-free processing (water-based separation), and ultra-low heavy metal concentrations certified via batch CoA.
The humanization of pet care has driven exponential demand for clinical-grade animal nutrition. Formulations now mirror medical-grade human therapeutics: restricted-mineral renal diets, single hydrolysed protein GI formulas, and freeze-dried raw matrices enriched with omega-3 fatty acids for dermatological restoration.
Manufacturers capable of providing pharmaceutical-grade batch separation and strict clean-out protocols between production runs are capturing global market share.
A whitepaper analysis on advanced processing methodologies driving efficiency, shelf stability, and molecular integrity in modern protein factories.
One of the primary historical barriers to high-concentration protein supplements and gummies has been bitterness and astringency caused by free amino acids and hydrolysed peptides. Advanced micro-encapsulation coats active protein particles in a microscopic lipid or lipid-carbohydrate shell.
This barrier prevents premature dissolution in the oral cavity, effectively masking unpleasant flavor notes without requiring artificial sweeteners or excess sugar, while ensuring targeted release inside the digestive tract.
Freeze-drying (lyophilization) represents the pinnacle of raw protein preservation. By freezing the protein matrix and lowering environmental pressure, moisture is removed directly via ice sublimation, bypassing the liquid phase entirely.
This process preserves 98%+ of natural enzymatic structures, thermosensitive vitamins, and essential amino acid chains, yielding a shelf-stable product that rehydrates instantly while maintaining the nutritional profile of fresh, raw food inputs.
Quality verification has evolved beyond basic Nitrogen/Kjeldahl combustion testing, which can be fooled by non-protein nitrogen additives. Modern CE-certified manufacturing utilizes HPLC and LC-MS testing to isolate and quantify exact amino acid profiles.
This guarantees that every claim on the commercial label—whether 24g of active whey isolate or specific BCAA ratios—matches finished production batches with 99.8% precision.
Addressing the core technical, regulatory, and commercial inquiries raised by international procurement officers during factory qualification.
Partner with a trusted, CE-certified UK and global protein manufacturer. Speak directly with our technical formulation scientists and contract manufacturing directors.